
Loose Iron Chips Took Up Too Much Storage Space
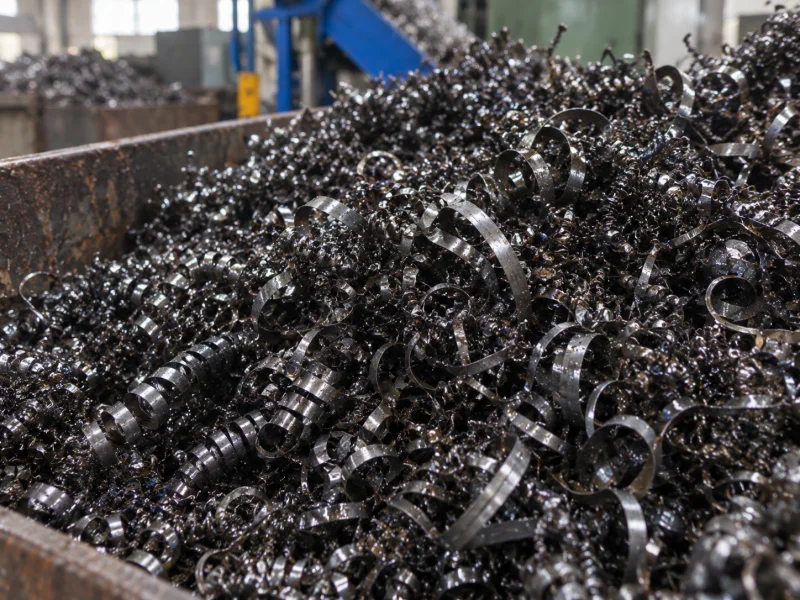
Iron chips occupy a large volume when stored loose, and the customer’s existing storage area was gradually becoming insufficient.
The customer is a machining company in Foshan, Guangdong, generating more than 50 tonnes of iron chips each month.
Before the project, the chips were collected continuously in the workshop and stored loose until the storage area was nearly full, at which point they were shipped out in bulk.
As production continued, the loose chips took up increasing amounts of storage space. Cutting fluid carried with the chips also added to housekeeping and cleanup work. At the same time, the customer wanted to reduce outbound transport costs and recover as much reusable cutting fluid as possible.
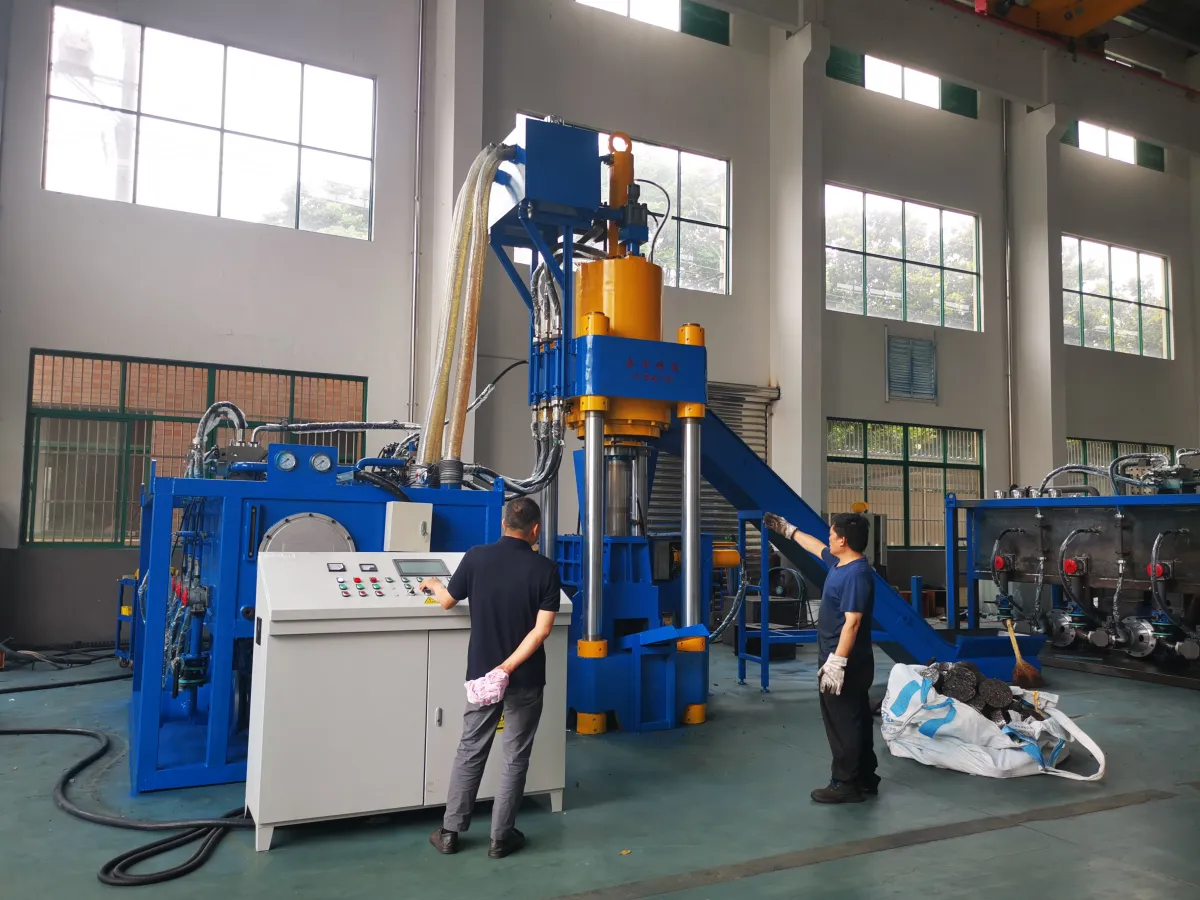
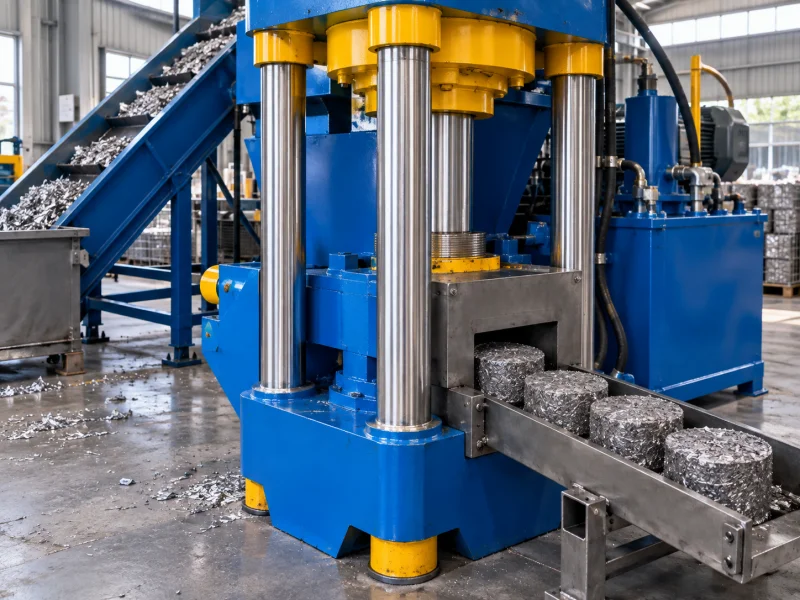
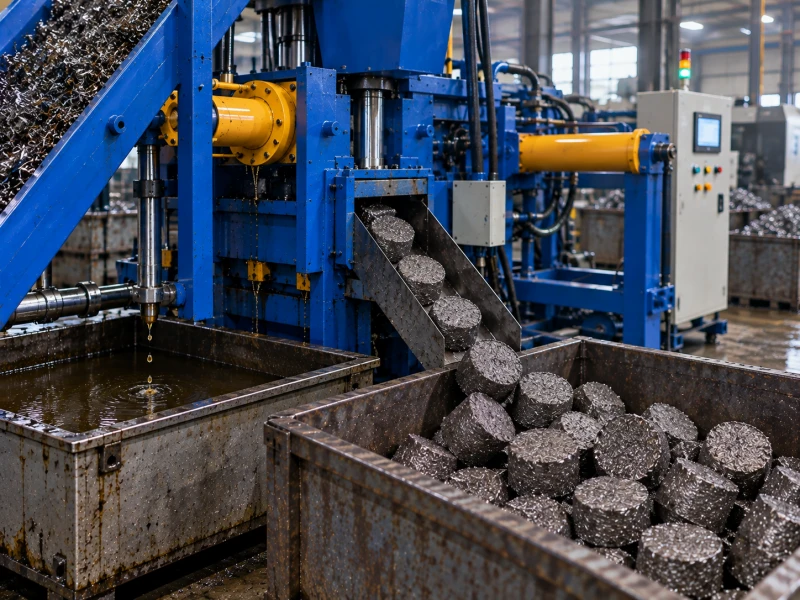
TITAN therefore configured a Y83L-630 Vertical Metal Chip Briquetting Machine together with a cutting fluid recovery tank. The machine presses the loose iron chips into compact briquettes under high pressure, while cutting fluid separated during pressing is collected in the recovery tank.
After the system went into operation, the storage space required for the iron chips fell to less than half its previous level. Transport costs were reduced by approximately CNY 80–120 per tonne, while the recovered cutting fluid could be reused.
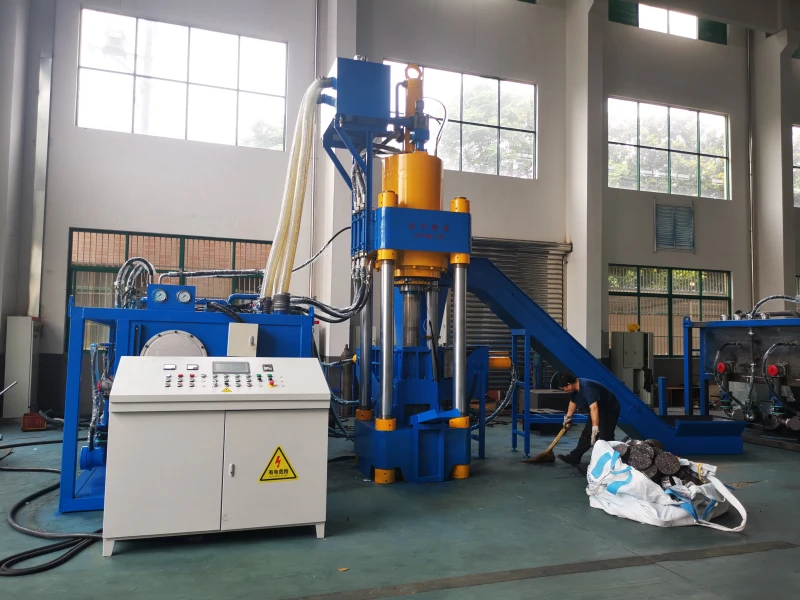
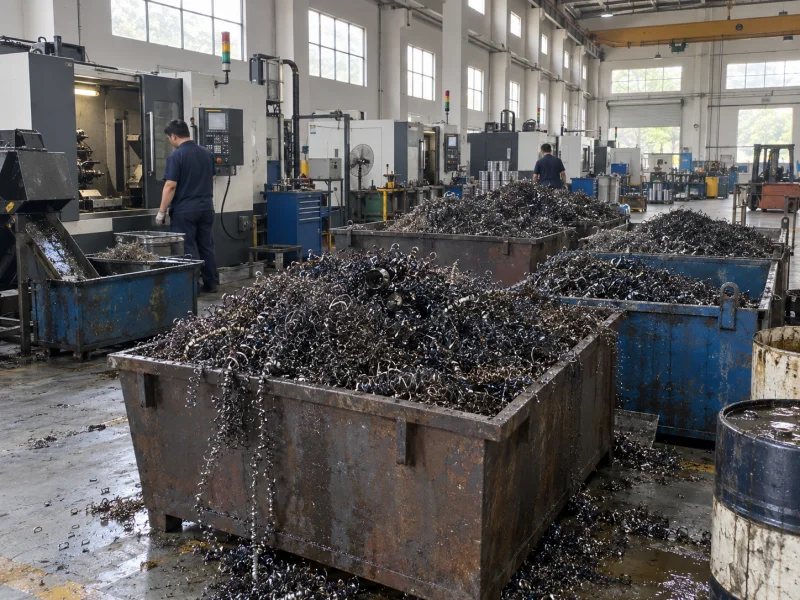
The customer continuously generates more than 50 tonnes of iron chips each month. Before briquetting, the material was stored loose and shipped out only after a sufficient quantity had accumulated.
As production volumes built up, simply allocating more storage space was no longer a sustainable solution.
Iron chips occupy a large volume when stored loose, and the customer’s existing storage area was gradually becoming insufficient.
The customer typically waited until enough chips had accumulated before arranging a bulk shipment. Because loose chips make inefficient use of available transport volume, transport cost per tonne remained high.
Machining chips carried residual cutting fluid, which could contaminate the workshop when the material was stored loose. The customer had also previously received environmental penalties related to site contamination.
When cutting fluid remained trapped in loose iron chips, it not only made material handling more difficult but also meant that recoverable fluid was being lost with the scrap.
The project therefore needed to address three issues together: volume reduction, transport efficiency, and cutting fluid recovery.
Because the customer continuously produces a large volume of iron chips, the project uses vertical briquetting as the main processing route.
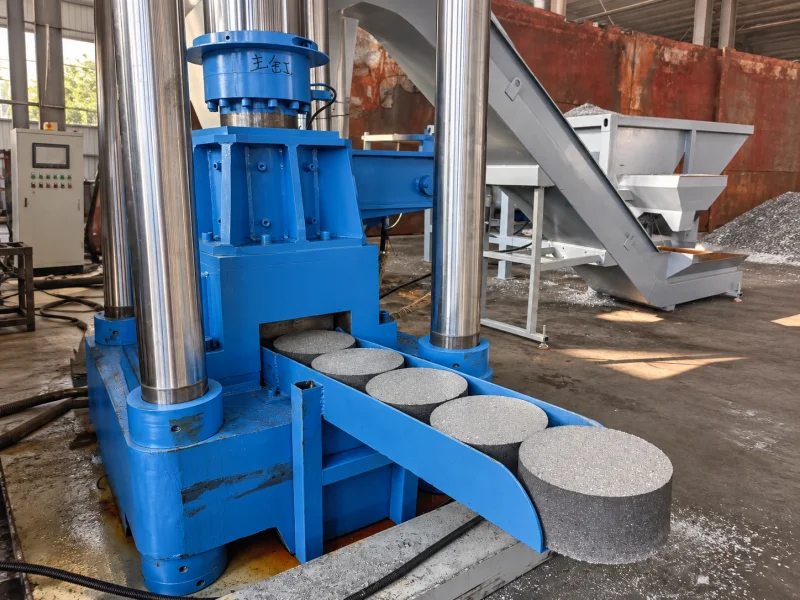
The loose iron chips are fed into the Y83L-630 and pressed under high pressure into compact briquettes. As the material is compressed, part of the cutting fluid separates from the chips and is directed into the recovery tank for collection.
This allows the customer to reduce the space occupied by the chips while improving cutting fluid handling within the same process.
The customer selected a Y83L-630 Vertical Metal Chip Briquetting Machine with a cutting fluid recovery tank to handle more than 50 tonnes of iron chips per month.
Under high pressure, the machine forms loose iron chips into compact briquettes. Cutting fluid separated from the material during pressing is directed into the recovery tank for collection.
In this project, the Y83L-630 was used primarily to reduce the storage volume of the iron chips, improve their condition for outbound transport, and recover cutting fluid through the supporting collection system.
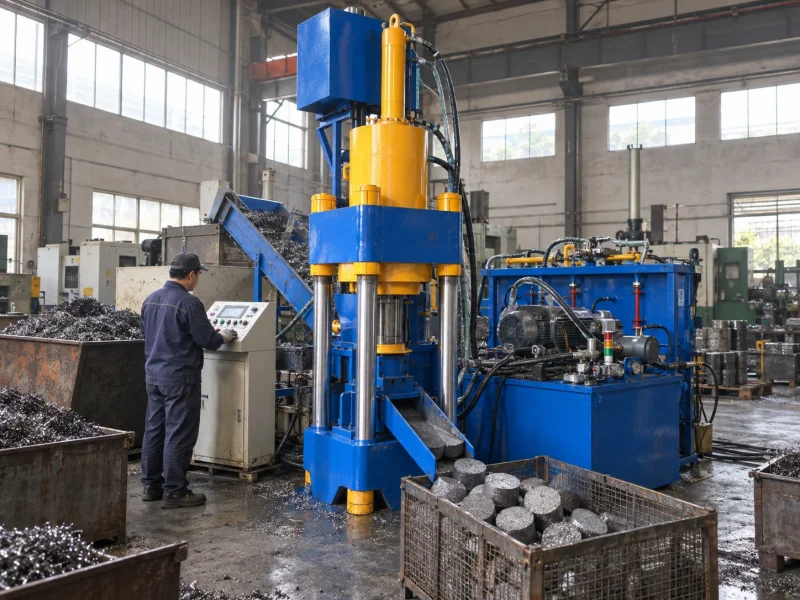
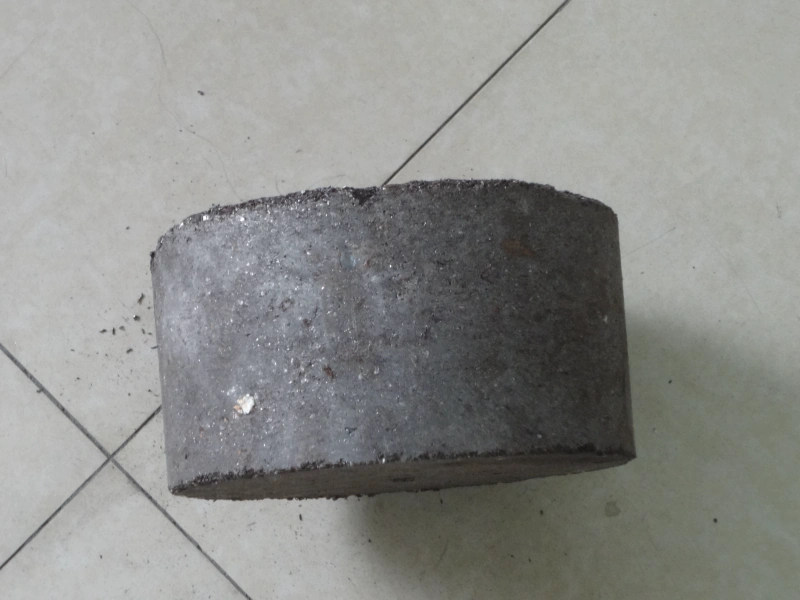
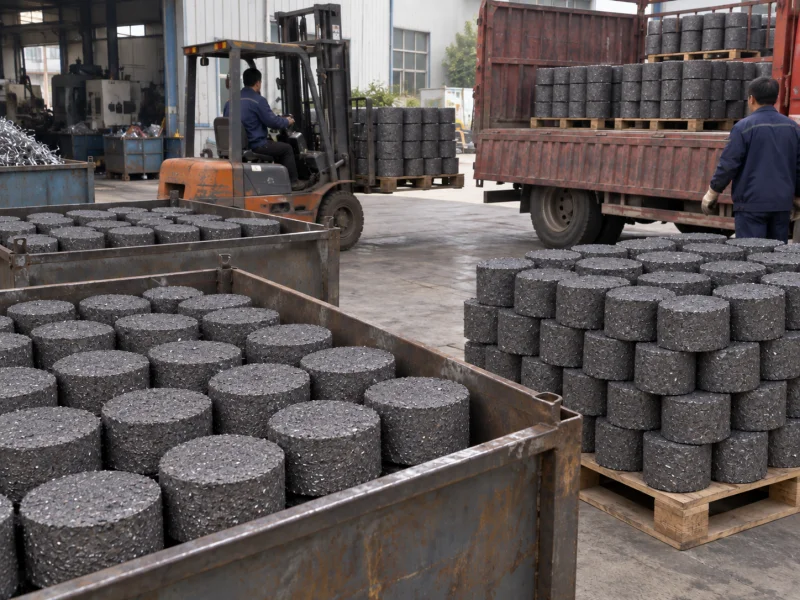
After the system went into operation, the Y83L-630 converted the loose iron chips into much more compact briquettes.
According to project records, the space required to store the processed chips fell to less than half the previous level, allowing the customer to keep more material within the existing storage area.
The denser form also improved outbound transport efficiency. Transport costs were reduced by approximately CNY 80–120 per tonne.
Cutting fluid separated during briquetting was collected in the recovery tank and could be reused, reducing fluid loss.
After the project went into operation, the iron chips required less than half the storage space used previously.
According to project records, transport costs were reduced by approximately CNY 80–120 per tonne of iron chips.
The customer generates and needs to process more than 50 tonnes of iron chips each month.
Cutting fluid separated during briquetting is collected in the recovery tank and can be reused.
Compacts loose metal chips into dense briquettes for easier handling, storage, transport, fluid recovery, and recycling.
View Equipment →Evaluate metal type, chip form, liquid content, contamination, and safety before selecting direct briquetting or the necessary pretreatment route.
View Solution →